Choosing material handling systems in 2026 requires more than comparing conveyor speeds or automation features. Warehouses now face changing order volumes, labor pressures, energy costs, and tighter delivery expectations. A system that performs well in a brochure may struggle with damaged cartons, uneven pallets, or seasonal demand.
Experienced operations teams begin with the physical reality of the site. They measure aisle widths, ceiling height, floor conditions, travel distances, and loading patterns. They also study the products themselves. Weight, dimensions, fragility, packaging quality, and storage temperature can change the right decision. A practical assessment should include process data, maintenance requirements, operator feedback, and future expansion plans. Small details matter.
A reliable selection process compares throughput, flexibility, safety, integration, energy use, and total ownership cost. It should examine how equipment connects with warehouse management software, sensors, robotics, and existing machinery. Site visits and controlled pilot tests often reveal problems that spreadsheets hide. No forecast is perfect. That deserves attention. Demand may shift, software integration may take longer, and staff training may require more time than expected. Independent engineering advice, supplier references, and documented performance data can reduce these risks. The strongest choice is not always the most automated option. It is the system that fits current workflows, supports measurable improvement, and can adapt without creating unnecessary complexity.
Choosing a material handling system in 2026 starts with a demanding question: what must it move during the busiest hour? Measure cartons, pallets, totes, weights, dimensions, travel distances, and order profiles from real operations. Do not size equipment around an average Tuesday. A peak wave can expose every weak point. Use observed data from seasonal promotions, shift changes, and replenishment delays. Then calculate required throughput, including scanning, loading, accumulation, and discharge time.
Plan for 20–30% growth beyond the peak requirement, not beyond today’s average. This allowance can absorb new product lines, higher order frequency, staffing changes, and layout constraints. For example, a system moving 1,000 cases per hour should be tested at 1,200 to 1,300 cases. Check whether motors, controls, lanes, and accumulation zones can sustain that rate without unsafe congestion. Ask operators to review the design. Their practical experience often reveals blocked aisles or awkward handoffs. Small details matter.
Reliable planning also needs stress testing. Model damaged cartons, mixed SKU sizes, late trailers, and short equipment stoppages. A design that works only under perfect conditions is not resilient. However, growth capacity should not become expensive idle space. Compare modular expansion with oversized equipment installed today. I have seen forecasts miss their target, even with careful spreadsheets. Review assumptions quarterly, record actual peak rates, and adjust the next investment with evidence. Leave room for correction.
Define 2026 requirements by sizing each process for peak throughput plus 20–30% growth capacity.
The chart uses a normalized peak workload of 1,000 units per hour. Required system capacity is calculated as peak throughput multiplied by 1.20, 1.25, or 1.30, helping prevent bottlenecks as demand increases.
Choosing a material handling system in 2026 starts with the load, not the equipment catalog. OSHA 1910.178 provides essential guidance for powered industrial truck operations, including capacity, stability, inspection, and operator training. It does not replace a site-specific engineering review.
Record each load’s weight, length, width, height, center of gravity, and packaging condition. A 900-kilogram pallet may seem routine until its contents shift during turning. A narrow crate can also create visibility problems. Measure the heaviest realistic load, not the average shipment. Include pallets, containers, attachments, and temporary packaging in the calculation.
Risk deserves equal attention. Rate loads as stable, shifting, fragile, liquid-filled, oversized, or difficult to see. Then compare those risks with aisle width, floor condition, travel distance, lifting height, and traffic levels. A system designed for uniform cartons may perform poorly with tall mixed pallets. Check rated capacities at the actual lift height and load center. Small details matter.
A clean spreadsheet can still be wrong. Recheck measurements during receiving, seasonal peaks, and product changes. Ask operators what happens during real shifts; their observations may expose hazards missing from drawings. Select controls such as load backrests, barriers, sensors, or slower travel zones only after identifying the specific risk. Leave room for human error. Even careful teams occasionally underestimate an awkward load.
| Load Class | Typical Weight | Typical Load Dimensions | Load Shape and Center of Gravity | Handling Risk | Recommended Handling System | Key OSHA 1910.178 Considerations | Pre-Selection Checks |
|---|---|---|---|---|---|---|---|
| Class 1: Light, Stable Unit Loads | Up to 500 lb (up to 227 kg) |
Up to 48 × 40 × 48 in (122 × 102 × 122 cm) |
Uniformly distributed, low center of gravity, securely contained or wrapped. | Low | Manual pallet truck, powered pallet truck, or light-duty stacker where travel distance and floor conditions justify powered equipment. | Operators of powered industrial trucks must be trained and evaluated as required by 29 CFR 1910.178(l). Equipment must be operated within its rated capacity. | Confirm floor condition, pallet integrity, travel distance, pedestrian interaction, and whether manual handling creates an ergonomic concern. |
| Class 2: Standard Palletized Loads | 501–2,000 lb (228–907 kg) |
Typically 48 × 40 × 48 in (122 × 102 × 122 cm) or smaller |
Stable palletized cartons, totes, drums, or containers with the load centered on the pallet. | Low to Medium | Powered pallet truck, walkie stacker, counterbalanced forklift, or reach truck selected for the required lift height and aisle width. | Use the truck’s rated capacity at the applicable load center and elevation. Loads must be stable, safely arranged, and properly positioned on the forks. | Verify gross weight, pallet condition, load center, rack height, aisle width, turning radius, ramp grades, and charging or fueling arrangements. |
| Class 3: Heavy or High-Capacity Loads | 2,001–5,000 lb (908–2,268 kg) |
Up to approximately 60 × 48 × 60 in (152 × 122 × 152 cm) |
Dense, compact loads such as machinery, metal components, bulk containers, or heavily loaded pallets. | Medium | Heavy-duty counterbalanced forklift or another powered industrial truck specifically rated for the load, attachment, lift height, and load center. | Capacity plates and markings must be present and legible. Attachments can reduce capacity and alter the effective load center; follow the truck and attachment manufacturer’s instructions. | Calculate the combined weight of load, pallet, and attachment. Check capacity at the actual load center, mast height, surface condition, and braking requirements. |
| Class 4: Extra-Heavy or Concentrated Loads | More than 5,000 lb (more than 2,268 kg) |
Varies; often compact or irregularly shaped | Very dense loads with concentrated weight, uneven weight distribution, or a load center significantly beyond the standard rating. | High | High-capacity powered industrial truck, engineered lifting system, or specialized load-handling equipment selected through a documented capacity review. | Do not exceed the rated capacity. The capacity must account for load center, lift height, attachments, dynamic forces, and the condition of the operating surface. | Obtain verified weight and dimensions; perform a lift-plan review; inspect floors, ramps, dock plates, storage locations, and clearance; restrict access where necessary. |
| Class 5: Long, Wide, or Oversized Loads | Any weight; commonly 1,000–8,000 lb (454–3,629 kg) |
Longer than 96 in, wider than 48 in, or extending beyond the pallet or fork envelope | Load may obstruct the operator’s view, shift laterally, or create an unusual load center. | High | Forklift with an approved attachment, side-shifting capability, or a suitable cart, crane, or engineered transport system. | Attachments must be approved for use and considered in the truck’s capacity. If the load obstructs forward visibility, the operator must travel with the load trailing or use an alternative safe method. | Measure total envelope, calculate the revised load center, define the travel route, control pedestrian access, and verify overhead and side clearances. |
| Class 6: Tall, Top-Heavy, or Unstable Loads | Typically 500–3,000 lb (227–1,361 kg) |
Height greater than 60 in (152 cm), or height-to-base ratio greater than approximately 1.5:1 |
High center of gravity, flexible packaging, liquid movement, stacked cartons, or an unsecured upper section. | High | Forklift or stacker with suitable mast height and capacity, combined with load stabilization, containment, or an engineered fixture. | Loads must be stable and safely arranged. Operators should avoid abrupt starts, stops, and turns and must follow safe travel practices and the truck’s operating limitations. | Assess tip-over potential, use stretch wrap or banding when appropriate, keep the load low during travel, and verify rack and storage stability. |
| Class 7: Fragile, Sensitive, or Spill-Prone Loads | Any weight; commonly 100–2,000 lb (45–907 kg) |
Any dimensions; often requires controlled orientation or limited acceleration | Glass, electronics, precision parts, liquids, or products sensitive to shock, vibration, tilt, or puncture. | Medium to High | Low-speed powered truck, cushioned or specialized attachment, secure container, or controlled conveyor and transfer system. | Powered industrial trucks must be operated safely and within their design limitations. Workplace conditions, visibility, pedestrian traffic, and load security must be addressed in training and operating procedures. | Define maximum acceleration, turning speed, tilt angle, and impact limits; inspect packaging; use secondary containment for spill-prone materials where required. |
| Class 8: Loads Requiring Special Attachments | Any weight within the combined rated capacity | Any dimensions; depends on the attachment and load interface | Rolls, coils, bales, cylinders, drums, cartons, or loads that cannot be safely supported by standard forks. | High | Powered industrial truck with an application-specific clamp, rotator, drum handler, fork extension, boom, or other approved attachment. | Attachments must be securely attached and used according to applicable capacity markings and instructions. The attachment’s weight and position can reduce truck capacity. | Confirm attachment compatibility, secure connection, revised capacity, load-center change, operator training, visibility, and the possibility of load release or rotation. |
| Class 9: Loads in Hazardous Locations | Any weight within the truck’s rated capacity | Any dimensions; location controls the equipment selection | Loads handled where flammable vapors, combustible dust, fibers, or other hazardous atmospheric conditions may exist. | High | Industrial truck specifically designated for the applicable hazardous location, or non-powered handling equipment approved for the environment. | 29 CFR 1910.178(c) addresses designations and use of powered industrial trucks in hazardous locations. Use only equipment appropriate for the classified location and hazard. | Identify the hazardous-location classification, ignition sources, ventilation, floor conditions, battery or fuel system requirements, and site-specific controls before selection. |
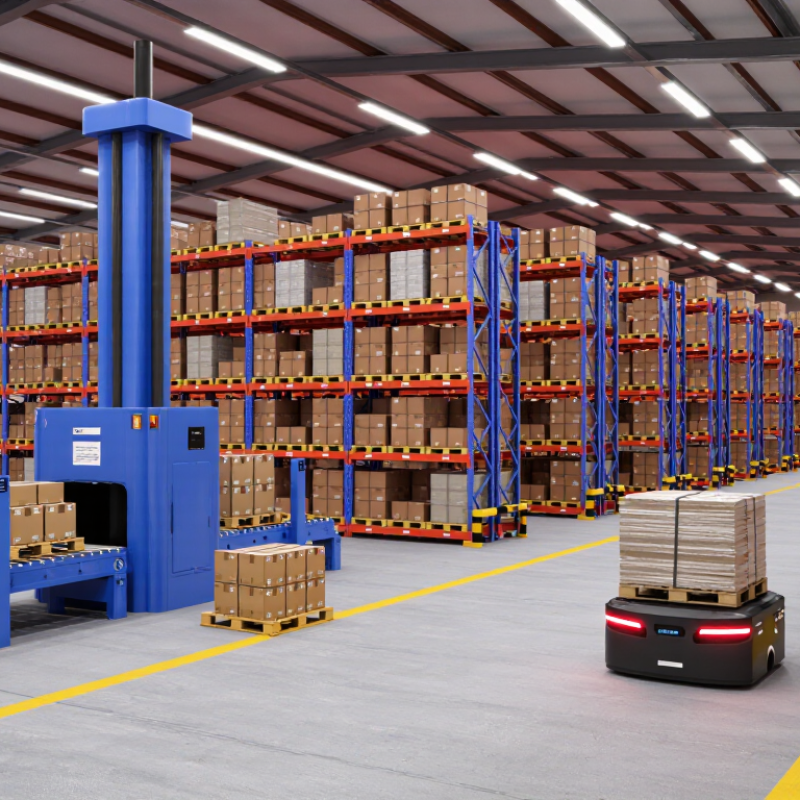
Accuracy, speed, and flexibility should guide the decision, not automation hype. Conveyors provide stable, predictable movement between fixed points. They suit repetitive flows, high volumes, and precise accumulation. However, changing a conveyor line can require costly mechanical work.
AS/RS systems offer excellent storage density and repeatable retrieval accuracy. They perform well when product dimensions and locations remain consistent. Their weakness is commitment. A poor sizing assumption can become an expensive bottleneck.
AMRs offer the greatest route flexibility. They can serve changing workstations, temporary storage areas, and seasonal demand. Yet, speed depends on traffic, battery charging, floor conditions, and software coordination.
A 2024 MHI Annual Industry Report found that 43% of surveyed supply-chain professionals currently use robotics and automation. The report also showed much higher expected adoption within five years. Demand is real, but readiness varies.
Compare measured outcomes, not brochures. A conveyor may win on sustained throughput. An AS/RS may win on space efficiency and retrieval consistency. An AMR fleet may win when layouts change weekly.
Interact Analysis has reported strong double-digit growth expectations for mobile robots, but market forecasts are not site guarantees. That distinction matters. Pilot one workflow, record cycle time, mispicks, congestion, and recovery time. Include exceptions. They often expose the real cost.
A hybrid design can be sensible, though integration complexity is easy to underestimate. Sometimes, a simpler conveyor remains the more reliable answer.
A reported 55% technology-spending trend signals stronger investment in warehouse automation. Yet spending more does not guarantee better performance. In 2026, choose systems around measurable constraints, not impressive demonstrations. Record order volume, SKU variety, aisle width, labor availability, and peak-hour congestion. These details expose the real operating problem.
A practical evaluation should compare conveyors, automated storage, mobile robots, sortation, and software coordination. Measure throughput, accuracy, uptime, maintenance hours, energy use, and payback period. Request performance data from similar facilities. Test integration with inventory and order systems before approving a full rollout. A small pilot can reveal delays that a polished presentation hides. Keep safety checks visible, including access controls, emergency stops, training, and inspection routines.
The 55% signal may encourage ambitious budgets, but technology should remain adjustable. Demand forecasts can fail. Product mixes change. A system sized for today’s peak may become expensive space tomorrow. I would reserve capacity for expansion, while avoiding automation that cannot operate during software outages. That balance is not perfect. It requires honest reviews after installation, using actual data instead of original promises. Smaller improvements, such as better slotting or clearer workflow design, may sometimes outperform a larger purchase.
Choosing a material handling system in 2026 requires more than comparing purchase prices. Validate the total cost across equipment, installation, training, energy, software, repairs, and downtime. A low-priced conveyor can become expensive when sensors fail or technicians wait for unavailable parts. Request five-year cost estimates with clear assumptions. Then test those figures against actual operating records.
Safety must be visible on the factory floor. Check reach distances, pinch points, emergency stops, noise, and pedestrian routes. Ask operators to review the proposed workflow. Their practical experience often reveals risks that drawings miss. Integration deserves equal attention. Confirm communication protocols, data ownership, cybersecurity controls, and compatibility with existing warehouse systems. Run a small pilot before approving a full rollout. It may expose uncomfortable gaps.
The business case should show a realistic three-to-five-year ROI, not an optimistic spreadsheet. Include labor changes, throughput gains, maintenance hours, rejected orders, and production interruptions. Use conservative volume forecasts. Sensitivity testing helps: what happens if demand falls 15 percent or energy costs rise? In one project review, an early model underestimated integration labor by nearly a quarter. That mistake changed the payback period. We should admit such uncertainty. A reliable decision includes contingency funds, measurable performance targets, service response times, and a review point after six months.